Categories
Blogs Mill Stands

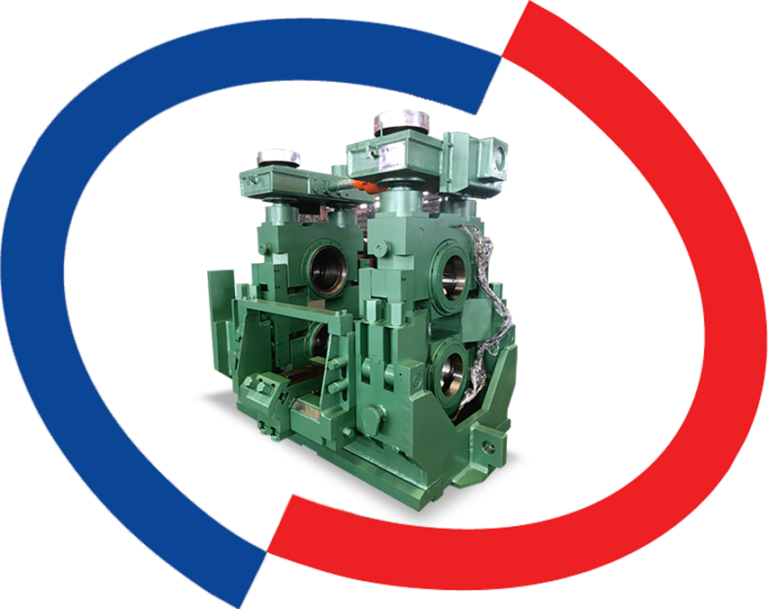
Walk down the line of a bar mill and every stand looks broadly alike: a housing, a pair of rolls, a spindle coming in from the drive. Yet the stand at the front of the mill and the stand at the back are doing very different jobs, and a plant that specifies them as if they were interchangeable usually pays for it later in broken rolls, unstable dimensions or constant stand changes. Understanding the roughing vs finishing mill stand distinction is the first step to specifying a rolling line properly.

The difference between roughing and finishing mill stands is the job each performs in the rolling sequence. Roughing stands take a hot billet through the first and heaviest reductions at low speed and very high load, while finishing stands make the last light reductions at high speed to deliver the final size, shape and tolerance. Intermediate stands bridge the two.

Nothing in that definition is complicated, but the consequences are. Each position in the train puts a different kind of stress on the stand, the drive and the rolls, and the design priorities change with it. This guide walks through the rolling sequence stand by stand, explains what each stage demands from the equipment, and finishes with the questions plant owners, engineers and procurement teams should ask a manufacturer before ordering.

The Rolling Sequence at a Glance

In a hot bar or section mill, a reheated billet passes through three groups of stands in order: the roughing train, the intermediate train and the finishing train. The bar is then cut, cooled and bundled. Published descriptions of continuous bar mills cite billets from about 130 mm square up to 250 mm square for larger lines, and the job of the whole train is to turn that thick, short piece of steel into a long, thin bar of exact dimensions.

Steel volume does not change as it is rolled, so every reduction in cross-section makes the bar longer. That single fact explains most of what follows. Take a 12-metre billet of 130 mm × 130 mm, which has a cross-section of 16,900 mm². A 16 mm round bar has a cross-section of roughly 201 mm². The same steel now stretches to about a kilometre in length, and it has to leave the last stand about 84 times faster than it entered the first. The front of the mill is slow, heavy and high-torque; the back is fast, light and precise. Every design difference between stands comes from that.

Most mills also alternate stand orientation, with horizontal stands followed by vertical ones, so the bar is squeezed from different directions without being twisted between passes. A rebar mill that Primetals Technologies announced for Pak Steel in 2021 shows the pattern clearly: a six-stand roughing train, a six-stand intermediate train and a four-stand finishing train, sixteen stands in all, built for an annual capacity of 450,000 tonnes. Your own mill may have fewer stands, but the logic is the same. Between the stands, roller table sections, guides and water boxes carry the bar from one pass to the next.

Stage Main Job Rolling Speed What Dominates the Design
Roughing Break down the billet with large reductions Lowest Shock load, torque, structural strength
Intermediate Bring the bar close to final section Medium, rising Balance of load and speed, flexibility
Finishing Set final size, shape and tolerance Highest Dimensional accuracy, rigidity, fast changeover

If you want the wider process picture, including reheating and cooling, our guide to the hot rolling mill process covers the full line. This article stays focused on the stands themselves.

Roughing Mill Stands

Role in the Sequence

The roughing mill in a steel plant is where the billet first meets the rolls, straight out of the reheating furnace and at its thickest. A roughing mill stand does the heavy lifting, taking large reductions per pass to turn a square billet into something much closer to the target proportions. The bar is still short and moving slowly, so the roughing stand in a rolling mill works at low speed but under the highest separating force and torque anywhere in the mill.

The front end of the bar is rarely clean, and the head and tail of a hot billet can be uneven. That is why crop shears are placed along the roughing section to trim the front and tail ends of the stock. Cobble shears sit ready to cut the bar up if a pass goes wrong. A roughing stand therefore has to survive the occasional bad entry, not just normal operation.

Design Priorities

Shock resistance and structural strength come first. A roughing stand sees the biggest load spike every time a billet bites, and a mis-fed or cold-ended billet makes that spike worse. Closed-type housings, cast or fabricated as a single rigid frame, are the usual choice for heavy roughing duty because they give the highest stiffness. Roll diameters are generally largest at this end of the line; published equipment specifications for re-bar mills commonly show diameters stepping down along the train, for example from around 560 mm in a roughing stand to around 410 mm in the first intermediate stands.

The drive line matters as much as the stand. Low speed and high torque mean a roughing stand relies on a robust reduction arrangement and well-matched rolling mill gearboxes, and an undersized drive shows up as stalled bars and cobbles rather than gradual wear. Because roughing rolls take the harshest treatment in the mill, serviceability matters more here than fine adjustment: this is where easy access and robust, repairable parts earn their keep.

Intermediate Mill Stands

Role in the Sequence

Intermediate stands take the roughed bar and reduce it, pass by pass, to a section that is near the final size. Loads are lower than in roughing, speeds are higher, and the bar is now long enough that it can span several stands at once. In a continuous mill that is where the line starts to behave as one connected machine, because each stand has to match the bar speed set by the one before it.

This is also the stage where mills gain or lose flexibility. On a plant that rolls several product sizes, the intermediate train is often where stands are added, bypassed or rearranged to suit the section being made. Published bar-mill layouts show intermediate trains split into groups, with stands that can be swapped to suit the range of finished sizes.

Design Priorities

An intermediate mill stand has to balance strength against speed. It needs enough rigidity to hold section accuracy as the bar gets smaller, but it also needs to run faster than a roughing stand without the stand and the bar misbehaving. Drive arrangement is a real design choice here: some mills drive stands in groups from a common motor, while others give individual stands their own drives for tighter speed control between passes.

Alignment and guide setup deserve particular attention. Small errors that go unnoticed in roughing are magnified as the bar gets thinner and faster, so intermediate stands reward accurate machining of housing windows and consistent roll chock fit. For that reason, how the stand was built matters as much as how it was specified.

Finishing Mill Stands

Role in the Sequence

The finishing mill stand is the last place the bar is shaped, and in practice it is where your customer’s tolerance is won or lost. Reductions here are light; the point is accuracy, not size reduction. The bar is long, fast and thin, and for TMT bar production it goes into the quenching and self-tempering section directly after the last stand, so whatever the finishing stand delivers is what the bar will be sold as.

Speeds in the finishing section can be very high. In wire rod mills, finishing blocks of six, eight or ten stands on a common drive are the conventional layout, and published designs describe delivery speeds above 100 m/s for thin rod. Bar and TMT mills run far slower, but the principle holds: the finishing stands are the fastest, lightest-loaded and most accuracy-sensitive in the line. A long, fast bar also needs the stand to hold alignment under vibration, since any looseness shows up directly as dimensional variation.

Design Priorities

Rigidity and repeatability lead the list. Finishing stands are where housingless mill stands make the strongest case. A pre-stressed housingless design limits roll spring-back, keeps the roll gap steady under load and allows a complete roll cartridge to be swapped quickly, which shortens the downtime of a changeover. Because size changes and roll wear show up first at the finishing end, fast stand changing tends to pay back here more than anywhere else in the mill.

Downstream equipment is tied to the finishing stand too. Once the bar leaves the last stand it is divided to length by a flying shear before it reaches the cooling bed, so the finishing section, the shear and the quenching line have to be specified as one sequence rather than three separate purchases.

Roughing vs Finishing Mill Stand: How Stand Design Changes Across the Sequence

Put the three stages side by side and the pattern is clear. Down the whole rolling mill stand sequence, load falls, speed rises and the price of an error shifts from broken equipment to out-of-tolerance product.

Design Factor Roughing Stand Intermediate Stand Finishing Stand
Typical load per pass Highest Moderate Lightest
Rolling speed Lowest Rising Highest
Frame preference Heavy closed-type housing for stiffness Conventional or housingless, depending on product range Housingless or high-rigidity frames for accuracy and quick change
Drive emphasis Torque and shock capacity Speed matching between passes Speed stability and fine control
Main failure risk Cobbles, broken rolls, overload Alignment drift, uneven wear Dimensional variation, rapid guide wear
What buyers should prioritise Strength and serviceability Flexibility and machining accuracy Rigidity and changeover speed

This classification works along a different axis from the one used to describe roll configuration. Two-high, three-high or four-high layouts, and conventional versus housingless frames, describe how a stand is built, and we cover them in our guide to the key components of mill stands. Roughing, intermediate and finishing describe where a stand sits in the line. A real specification needs both answers for every stand.

What to Ask Before Specifying Stands for Each Stage

Most mistakes in stand selection come from specifying the whole train from a single template. These questions help a plant owner, engineer or procurement lead keep each stage honest:

  • What billet size and steel grade will the roughing stand actually see? A mill planned around a larger billet needs more roughing capacity than the same product rolled from a smaller one.
  • What is the full product range? The smallest and largest finished sizes decide how many stands are needed and which ones must be easy to swap.
  • What is the target output in tonnes per hour? Output sets the speed the finishing stands must sustain.
  • Which stands need housingless designs and which can stay conventional? The answer is rarely the same for every stand.
  • How long does a stand or roll change take at each position? Changeovers tend to happen most often at the finishing end, so they deserve the closest attention.
  • What spares will be held for each stage? Wear parts at the front of the mill are very different from those at the back.

The Steefo Group designs and manufactures conventional, housingless and HV (horizontal-vertical) mill stands for hot rolling lines, built around the product range and output of each plant rather than a single catalogue size. If you are planning a new line or upgrading an existing one, our engineering team can help you match stand type and drive to each stage of the train. You can see the full range on our mill stands page or contact the team with your billet size and product range.

The roughing vs finishing mill stand question is really a question about where stress lands in the line. Roughing stands absorb the shock and torque of heavy reductions, intermediate stands carry the bar to near-final size while balancing load and speed, and finishing stands protect accuracy at the highest speed in the mill. Plants that specify each stage for the job it actually does, and not as a copy of the stand next to it, spend less time on unplanned stoppages and hold tolerance far more reliably.

Frequently Asked Questions

What is the difference between roughing and finishing mill stands?

Roughing stands make the first, heaviest reductions on a hot billet at low speed and very high load. Finishing stands make the final light reductions at the highest speed to set the product’s size, shape and tolerance. Intermediate stands sit between the two and bring the bar close to its final section.

How many stands are in a typical roughing, intermediate and finishing train?

It depends on billet size, product range and output. One published rebar mill design pairs a six-stand roughing train with a six-stand intermediate train and a four-stand finishing train. Smaller re-rolling mills usually use fewer stands, and larger or multi-product lines use more.

Why do rolling mills alternate horizontal and vertical stands?

Alternating horizontal and vertical stands squeezes the bar from different directions without twisting it between passes. This keeps the section stable, allows larger reductions and reduces wear on guides, which is why many housingless and HV stand arrangements are used in modern bar mills.

Can the same mill stand design be used for roughing and finishing?

Not usually. Roughing stands need heavy frames and drives built for shock and torque, while finishing stands need rigidity, repeatable alignment and fast changeover at high speed. Using one design for both tends to compromise one end of the line, and a stage-by-stage specification is the safer approach.

Does Steefo supply mill stands for every stage of a rolling line?

Yes. Steefo designs and manufactures conventional, housingless and HV mill stands, matched to the billet size, product range and output of each plant. Share your mill details with our engineering team and we will recommend the stand type and drive arrangement for each stage.

Get in Touch

To discuss stand selection for your roughing, intermediate or finishing train, call us at +91 98240 76873 or write to marketing@thesteefogroup.com.
Categories
Blogs Mill Stands

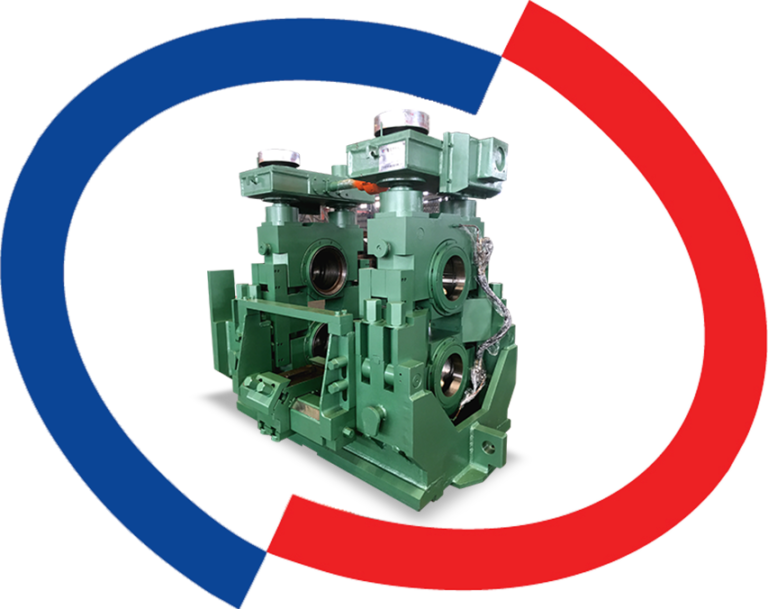
A mill stand carries the full rolling load of a hot rolling mill — every pass, every shift, for years without failure being an option. When a plant evaluates a new supplier, the question isn’t just what the stand costs; it’s how it was actually built, because that manufacturing process is what determines whether the stand holds tolerance under repeated high-load cycles or develops play and misalignment within a few years.

Mill stand manufacturing is the process of converting raw material — cast iron, cast steel, or fabricated steel plate — into a finished housing and roll-assembly structure through pattern-making, casting or fabrication, precision machining, assembly, and load testing, following a sequence that determines the stand’s final rigidity and alignment accuracy.

The process a manufacturer follows directly determines the stand’s rigidity, alignment accuracy, and service life under continuous rolling loads.

This guide walks through how rolling mill stands are actually manufactured — material selection, the production process step by step, and the quality checks a stand must pass before it leaves the factory — so you know what to ask when evaluating a manufacturer.

This matters more for structural and TMT bar mills running continuous multi-shift production than it might for lighter-duty applications, because a stand here rarely gets a genuine break between passes. The manufacturing decisions made before a stand ever reaches the mill floor are what determine whether it holds tolerance through years of that duty cycle or begins drifting within its first eighteen months.

Why Manufacturing Quality Determines Mill Stand Lifespan

A mill stand’s job is to hold two rolls in precise alignment while resisting the separating force generated as steel passes between them — a force that runs into hundreds of tonnes on a structural or TMT bar mill. If the housing flexes even slightly under that load, roll alignment drifts, and the result shows up downstream as dimensional inconsistency in the finished bar.

This is why manufacturing quality isn’t a finishing-touch consideration — it’s structural. A stand cast with internal porosity, or machined without verifying squareness between the housing windows, may pass a basic visual inspection and still fail to hold tolerance once it’s under real rolling load for a few months.

The practical consequence shows up gradually rather than as a sudden failure, which is part of why it’s easy to underweight at the ordering stage. A stand with a marginal casting defect or slightly out-of-tolerance housing window typically performs acceptably for the first few months. Wear then accelerates at the point of weakness, roll alignment drifts a little further with every pass, and by the time it shows up as a quality problem in the finished bar, the root cause is buried months in the past — and far harder to trace back to a manufacturing decision than it would have been to catch with proper testing before dispatch.

Material Selection for Mill Stand Fabrication

The starting material determines both the manufacturing route and the stand’s long-term behavior under load.

Cast Iron vs Cast Steel vs Fabricated Steel

Cast iron housings are common on lighter, older mill designs — they’re straightforward to produce in a single-piece pour but carry more risk of internal casting defects and generally lower toughness than cast steel. Cast steel housings, used widely on modern roughing and intermediate stands, offer significantly better toughness and resistance to shock loading, which matters when a mill trips or an oversized billet enters the pass. Fabricated steel housings — welded from forged steel plate rather than cast in one piece — skip the pattern-and-mold stage entirely, which shortens lead time and avoids casting-related defects, at the cost of requiring precise weld sequencing to control distortion.

The choice isn’t purely a cost decision. A roughing stand absorbing the highest separating forces in the mill is generally better served by cast steel’s toughness, while a finishing stand — handling lighter loads but requiring tighter dimensional accuracy — can sometimes be well served by a fabricated design if weld quality and stress-relief are properly controlled. Reputable manufacturers select the route based on the stand’s position in the rolling sequence, not a single default material across the whole mill.

Closed-type housings, cast as a single rigid frame, are generally specified for heavy roughing stands where maximum stiffness matters most. Open-type housings, with a removable top cap, trade a small amount of rigidity for significantly faster roll-change time — a relevant factor for mills running frequent product changeovers.

The Manufacturing Process Step-by-Step

Regardless of material route, a mill stand goes through the same broad sequence before it’s ready to ship.

Pattern-Making & Casting (or Fabrication)

For cast housings, a pattern is produced first — traditionally in wood or resin, increasingly via CAD-driven pattern design — and used to create the sand mold the housing is poured into. For fabricated housings, forged steel plates are cut to profile and prepared for welding according to a controlled sequence designed to minimize distortion.

Stress Relief

Both cast and welded housings carry internal stresses from the casting or welding process itself — stresses that, left unaddressed, release slowly over time and cause dimensional movement after the stand is already machined and in service. Heat-treatment stress relief before machining is what prevents this, and it’s a step that’s straightforward to skip under time pressure but difficult to detect until the stand is already installed and drifting.

Machining & Precision Boring

Once the rough casting or weldment has stress-relieved, it moves to machining, where the critical surfaces are cut to final dimension: the housing windows that locate the roll chocks, the base mounting faces, and the bores for adjustment screws. This is the stage where tolerance is actually created — a housing window bored even a fraction of a millimeter out of parallel will show up as uneven roll wear later.

Assembly & Fitting

Roll chocks, adjustment mechanisms, and bearing housings are fitted into the machined stand and checked for free movement without play. On stands with screw-down or hydraulic adjustment, this stage also confirms the adjustment mechanism moves through its full range without binding.

Quality Checks & Testing Before Dispatch

A mill stand that looks correct on the shop floor still has to prove it under conditions that approximate actual rolling load before it’s cleared for dispatch.

Dimensional Accuracy Checks

Housing window parallelism, base flatness, and bore alignment are verified against drawing tolerances using coordinate measuring or precision gauging — not just a visual and tape-measure check. For stands manufactured for TMT bar and structural mills, this verification directly determines whether the finished bar will meet dimensional tolerance once the stand is installed.

Material & Load Testing

Cast components are checked for internal defects — porosity, shrinkage cavities, or cracks — typically through ultrasonic or dye-penetrant testing on critical load-bearing sections. Material certificates confirming the correct grade and heat treatment should accompany every stand, and a reputable manufacturer will provide these without being asked.

Some manufacturers go further and simulate service load on a test rig before dispatch, checking for deflection under a controlled force approximating the stand’s rated separating force. This isn’t universal practice — it adds time and cost to the manufacturing cycle — but for a Tier-1 structural component like a roughing stand, it’s the closest a buyer can get to proof of performance before the stand is actually installed and running production.

What to Ask Your Mill Stand Manufacturer Before Ordering

Before finalizing an order, ask specifically: what material grade and casting or fabrication method is used for this stand type, what dimensional tolerances are held on the housing windows, and what testing (ultrasonic, dye-penetrant, load testing) is performed before dispatch. A manufacturer with a mature quality process will have specific, documented answers to all three — vague reassurance is itself a signal worth noting.

It’s also worth asking how the manufacturer’s stand design interacts with your specific mill stand configuration — housingless designs are manufactured and machined differently from conventional closed housings, and a supplier experienced with both will be able to explain the trade-off for your application rather than defaulting to whichever they build most often.

Question What a Strong Answer Looks Like
Material grade & route Specific grade (e.g., cast steel to a stated specification) with a documented reason for the choice given your mill type
Dimensional tolerance held Numeric tolerance figures for housing window parallelism and bore alignment, not “high precision”
Pre-dispatch testing Named tests performed (ultrasonic, dye-penetrant, load test) with certificates provided as standard
Lead time & capacity A specific timeline tied to your stand configuration, not a generic range

Understanding how a mill stand is actually manufactured changes the conversation with a supplier from “what does it cost” to “what am I actually getting for that cost.” The stands that hold tolerance for years under continuous rolling load are the ones where material selection, machining precision, and pre-dispatch testing were treated as engineering requirements, not finishing steps. That’s the standard worth asking every mill stand manufacturer to meet.

Frequently Asked Questions

What material is best for rolling mill stand housings?

It depends on the application. Cast steel offers the best combination of toughness and rigidity for most roughing and intermediate stands, while fabricated steel housings can offer shorter lead times for certain configurations. Cast iron is still used on lighter or older mill designs but generally offers lower shock resistance than cast steel.

How long does it take to manufacture a mill stand?

Lead time depends on the housing type, size, and whether it’s cast or fabricated. Cast housings typically require longer lead times due to pattern-making and casting stress-relief, while fabricated housings can sometimes be produced faster since they skip the mold stage entirely.

What quality tests should a mill stand pass before dispatch?

At minimum, dimensional accuracy checks on housing windows and mounting faces, plus material integrity testing — ultrasonic or dye-penetrant inspection — on critical load-bearing sections. Material certificates confirming grade and heat treatment should be provided with every stand.

Why do some mill stands lose alignment after a few years of use?

This is usually traced back to the manufacturing stage rather than operational wear alone — internal casting defects, insufficient stress-relief before machining, or housing windows machined outside tolerance all show up over time as drift in roll alignment under sustained load.

Does Steefo manufacture custom mill stands for specific mill configurations?

Yes. Steefo designs and manufactures mill stands — including housingless and conventional configurations — matched to a plant’s specific rolling requirements. Contact our engineering team with your mill configuration for a tailored specification.

Get in Touch

To discuss a mill stand manufacturing specification for your rolling mill, see how our stands are engineered on the mill stands product page, read more on what sets our stands apart in The Steefo Advantage: Mill Stands Built to Last, or reach out to our team directly. Call us at +91 98240 76873 or write to marketing@thesteefogroup.com.

Categories
Blogs Rolling Mill

Demand for high-strength Thermo Mechanically Treated (TMT) bars is surging across the global construction sector. From towering residential skyscrapers to massive public infrastructure projects, the market requires unparalleled volumes of structural steel. This creates immense daily pressure on steel plant managers and floor operators. The objective is clear and relentless. Facilities must push for maximum daily output without ever compromising the structural integrity or quality of the steel.

Older manufacturing setups struggle significantly under these harsh, modern demands. Traditional heavy frames create severe bottlenecks and precision issues during continuous, high-speed production runs. The huge cast iron housings found in older equipment stretch and flex under heavy loads. This flexing leads to gauge variations, causing the final TMT bars to fall outside strict weight and dimensional tolerances. When precision drops, profitability immediately follows.

The core solution for overcoming these industrial bottlenecks lies in modern mechanical upgrades. Switching your primary equipment to a housingless mill stand is the most reliable way to guarantee uniform TMT bar dimensions. Furthermore, this specific upgrade drastically cuts down on expensive plant downtime. The modern engineering behind these units transforms how a heavy manufacturing facility operates daily.

The Engineering Behind Modern TMT Manufacturing

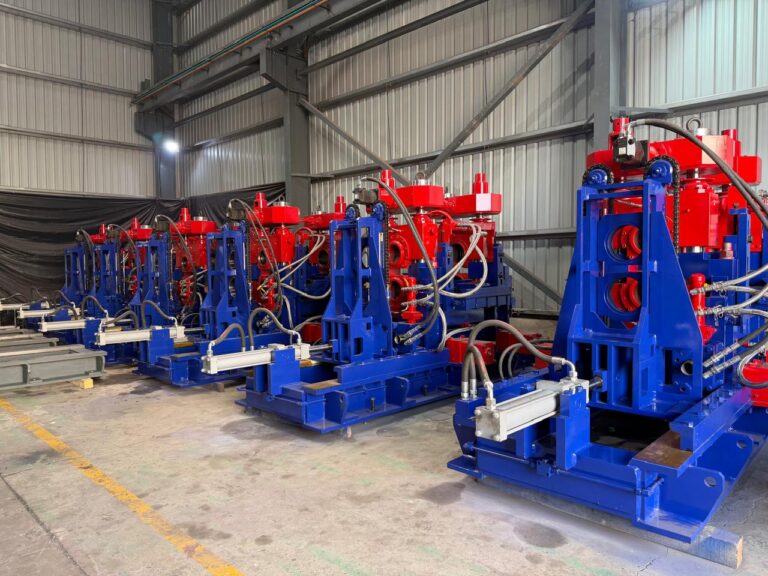
Understanding why a housingless mill stand outperforms legacy equipment requires a close look at its stripped-down, highly efficient design. This industrial unit entirely removes the outer cast housing that defines conventional setups. Instead of relying on a bulky, heavy frame to contain the rolling forces, the roll chocks connect directly to each other via high-strength, pre-stressed tension screws. This creates an incredibly rigid and compact rolling module. The top and bottom chocks are locked together firmly, ensuring the rolls remain where they need to be during heavy operation.

The fundamental engineering principle driving this efficiency is the short stress path. In traditional mill stands, the extreme separating force generated by the hot steel billet travels through a long route. It moves from the rolls to the chocks, up the pressure screws, into the cast housing, and finally back down. This long path acts like a giant, heavy spring. Under extreme pressure, the housing stretches slightly. This elastic stretch causes the rolls to part, which ruins the dimensions of the steel.

A housingless mill stand dramatically shortens this stress path. The intense rolling force only travels through the rolls, the chocks, and the immediately connecting tension screws. A shorter stress path means the machine absorbs rolling forces far more effectively than conventional equipment found in older rolling mills. Because the tension screws are short and highly rigid, their elastic elongation is practically zero. This eliminates the mill spring effect.

How a Housingless Mill Stand Upgrades TMT Bar Quality

The precision that a housingless mill stand provides translates immediately into superior steel products. Upgrading your facility guarantees three direct improvements to the final product.

1. Attain High Dimensional Accuracy

Minimal roll deflection keeps the hot metal exactly within the required tolerance from the very first pass. Traditional rolling mills often produce bars that are slightly overweight due to roll parting under load. This forces manufacturers to give away free steel to meet minimum length requirements. The hyper-rigid design of a housingless mill stand eliminates this costly issue. The rolls hold their gap under maximum load. This extreme dimensional accuracy is a non-negotiable factor for standard TMT ribbed profiles to meet strict international building codes.

2. Guarantee Uniform Metal Deformation

Inside a housingless mill stand, the structural rigidity ensures flawless shaping. The hot steel billet gets shaped perfectly and evenly from the first roughing pass to the final finishing block. Uniform deformation is critical for the internal grain structure of the metal. When the steel is compressed evenly, its tensile strength and yield strength become highly consistent across the entire length of the bar. There are no weak spots or uneven zones caused by mechanical flex.

3. Deliver a Flawless Surface Finish

Consistent pressure across the highly stable rolls prevents structural flaws on the final steel bars. Any vibration or shifting in traditional mill stands can cause surface tearing, uneven rib formation, or lap defects. By eliminating mechanical play, the rolls bite the steel smoothly. This guarantees that the transverse ribs—which are essential for concrete bonding in construction—are formed at the required depth and spacing.

Drive Plant Floor Efficiency

Beyond product quality, incorporating a housingless mill stand on the floor revolutionises operational speed. The focus shifts strictly to the speed of maintenance and uninterrupted running times.

Unplanned production stops are the biggest profit drain in modern steel plants. Every minute a line sits idle, the facility bleeds potential revenue. Traditional setups require hours of manual labour to fix issues or adjust guides. In contrast, modern equipment is designed to keep the red-hot steel moving at maximum velocity. Fast maintenance protocols ensure that the line rarely stops for long.

The mechanics of quick roll changes completely transform the shift changeover process. In older facilities, changing worn rolls meant shutting down the line and dismantling heavy components right on the floor. Every modern housingless mill stand supports an offline standby method. While the active unit is running, floor staff prepare the next unit in the workshop area. When a roll change is required, operators disconnect a single utility plate. An overhead crane lifts the entire spent module out of the line and drops the pre-aligned new unit into place. This turns an exhausting two-hour mechanical swap into a swift fifteen-minute procedure.

This speed directly maximises continuous rolling operations. Modern equipment handles incredibly long production runs without needing constant manual adjustments from the floor staff. Because the rolls do not flex or part, operators do not have to constantly tweak the screw-down mechanisms to compensate for wear or gauge variation. The machine simply runs seamlessly until the scheduled changeover time.

Mechanical Superiority and Equipment Longevity

Every housingless mill stand engineered for heavy industry is built to survive brutal conditions while protecting its most delicate internal components.

Better load distribution directly protects the internal bearings from premature failure and excessive wear. Heavy-duty spherical roller bearings or multi-row cylindrical bearings sit inside the chocks. Because the short stress path prevents the rolls from bending, the load on these bearings remains perfectly even. There is no edge-loading or twisting force applied to the bearing races. This extends bearing life under heavy loads significantly, saving plants lakhs of rupees in replacement parts every quarter.

Furthermore, these modern units excel at eradicating backlash. A housingless mill stand features self-balancing spindle mechanisms and automated screw-down features. Traditional setups often suffer from mechanical play between the threads and the chocks. When the steel billet hits the rolls, this gap snaps shut, causing a shockwave through the machine. Modern roll balance systems use powerful hydraulic cylinders to keep the chocks constantly pressed against the screw-downs. This completely prevents mechanical play or shock during heavy operation.

Finally, operators benefit from built-in automated utility connections. Built-in hydraulic lines, grease lubrication channels, and water cooling mechanisms are routed through a single multi-coupling block. This automated defence protects the machinery automatically without relying on operators to manually connect dozens of individual hoses. If a line needs to be swapped, the utilities disconnect and reconnect flawlessly in seconds.

Optimise Steel Plant Layout

Integrating new machinery into an existing industrial space is often a logistical nightmare. However, installing a housingless mill stand offers plant managers incredible flexibility.

1. Adapt to Compact Footprints

A housingless mill stand requires significantly less floor space compared to bulky traditional frames. By removing the giant cast iron housing, the overall volume of the machine shrinks by nearly half. This allows steel manufacturers to fit more rolling passes into a shorter building. It also frees up vital floor space for safer operator walkways and better material handling logistics.

2. Leverage Horizontal and Vertical Configurations

Modern mills must eliminate the twisting of the hot steel bar between passes. Twisting causes surface defects and slows down the line speed. These modern units offer the flexibility of being installed in alternating horizontal and vertical configurations. The universal design allows the same base cartridge to operate perfectly in either orientation to perfectly suit the existing mill setup.

3. Integrate Seamlessly Into Existing Lines

Plant managers do not need to completely rebuild their facility to see immediate benefits. Upgrading specific weak points in a line is highly viable. You can seamlessly replace an ageing finishing block with a continuous train of these advanced units. The compact base plates can be engineered to fit precisely onto your existing foundations.

Track the Financial Returns of a Housingless Mill Stand Upgrade

Ultimately, upgrading to a housingless mill stand translates into significant financial gains across three major operational pillars.

First, these units actively lower annual maintenance budgets. The extended component lifespan of high-end bearings and the vast reduction in moving parts lead to direct annual cost savings. There are no housings to inspect for micro-fractures. The offline maintenance model means fewer tools and fewer emergency mechanical interventions on the hot floor.

Second, this equipment directly boosts overall production capacity. Faster roll changes mean the line operates for more hours every single week. Continuous running without manual gauge adjustments directly increases the total daily tonnage of finished TMT bars. Capturing an extra hour of rolling time per day yields substantial revenue increases over a fiscal year.

Finally, facilities experience noticeable reductions in energy consumption during operations. Because a housingless mill stand operates with incredibly low friction and zero mechanical binding under load, it draws far less power. The main drive motors do not have to fight against the internal flexing of the machine. This highly efficient design lowers the electrical draw during heavy metal deformation cycles, shrinking the plant’s monthly utility overhead.

Conclusion

The implementation of a housingless mill stand represents the peak of modern hot rolling technology. The construction industry will only continue to demand higher volumes of flawless TMT bars. Steel plants relying on outdated, cast housings will inevitably face higher maintenance costs and lower production ceilings. By embracing the rigid, compact, and efficient engineering of modern tension-screw setups, plant managers can eliminate costly bottlenecks. From protecting bearing life to ensuring perfect dimensional accuracy, this equipment secures a plant’s profitability for decades to come.

Frequently Asked Questions

1. How does a Housingless Mill Stand improve TMT bar dimensions?

The rigid design relies on short tension screws rather than a large cast housing. This creates a very short stress path that prevents the rolls from flexing or parting under extreme pressure. This precise gap maintenance guarantees the final TMT bar matches exact weight and dimensional tolerances.

2. Why is the short stress path important for hot rolling mills?

A short stress path eliminates mill spring. It prevents the heavy rolling force from travelling through a large, elastic frame. Instead, the force is contained within a compact loop, allowing the machine to absorb heavy loads without distorting the final product.

3. Can we install a Housingless Mill Stand in our existing TMT production line?

Yes. These units are highly adaptable due to their compact footprint and versatile base designs. You can upgrade specific sections of your existing line without needing to rebuild the entire facility or pour entirely new foundations.

4. How much time is actually saved during a quick roll change?

Traditional setups can take hours to dismantle and reassemble on the floor. With the modern offline standby method, an overhead crane swaps an entire pre-assembled cartridge in roughly fifteen minutes. This gets the production line moving again almost instantly.

5. Does this equipment really reduce overall maintenance costs?

Absolutely. The design ensures better load distribution, which dramatically extends the lifespan of expensive internal bearings. Furthermore, the use of hydraulic roll balancing eradicates mechanical shock and backlash, significantly lowering the frequency of emergency repairs.

Upgrade Your TMT Production Line with The Steefo Group’s Advanced Housingless Mill Stands Today

Are you tired of costly downtime and inconsistent steel quality eating into your profits? The construction sector demands absolute perfection, and legacy equipment holds your capacity back. It is time to transform your floor efficiency.

At The Steefo Group, we engineer industry-leading solutions in Ahmedabad. Our highly rigid equipment eliminates mill spring, guarantees dimensional accuracy, and drastically slashes maintenance times. Stop worrying about roll deflection and start maximising your daily finished tonnage.

Partner with a manufacturer that understands the harsh realities of high-speed operations. We will help you integrate our robust units seamlessly into your existing layout.

Ready to boost your total output and secure a competitive edge? Contact The Steefo Group now. Speak with our technical experts at +91 87589 98607 or email us at marketing@thesteefogroup.com to request a custom quote.

Categories
Blogs Rolling Mill

Every mill manager knows the frustration of a finished product that just barely misses the mark. You run the steel through the line and check the gauge, but the tolerances are off by a fraction of a millimetre. You adjust the screw-down, run it again, and face the same inconsistency. It is a battle against physics that eats into your production time and increases your scrap pile. This struggle often comes down to one critical component. The “spring” effect in your heavy machinery is fighting against you.

For decades, the steel industry has relied on conventional equipment to get the job done. These massive iron giants have built the modern world. However, as market demands for precision tighten in 2026, reliance on older designs is becoming a liability. This brings us to the core conflict in modern rolling mills. You have the traditional, conventional stands that are familiar yet flawed, and you have the housingless stands that represent the future of rolling technology.

Upgrading to housingless mill stands is not just about buying shiny new gear or keeping up with trends. It is a calculated strategic move. It is about securing higher precision, drastically lowering your operational costs, and ensuring your steel plant remains competitive in a market that no longer forgives inefficiency.

What Defines the Two Technologies

To understand why an upgrade is necessary, we must first look under the hood of these two distinct technologies. The difference is not just in how they look but in how they handle the immense forces of rolling steel.

Conventional Mill Stands

The conventional mill stand design has been the standard in rolling mills for over a century. These stands are characterised by their massive size and weight. They rely on heavy cast steel closed housings to contain the roll chocks. In this design, the chocks slide vertically inside the housing window to adjust the roll gap.

While they look indestructible, their sheer size is actually part of their limitation. The stress path travels through the long housing posts. The chocks are not rigidly fixed but float within the window with certain clearances. This design was sufficient when tolerance requirements were loose, but it struggles to meet the strict standards of today.

Housingless Mill Stands

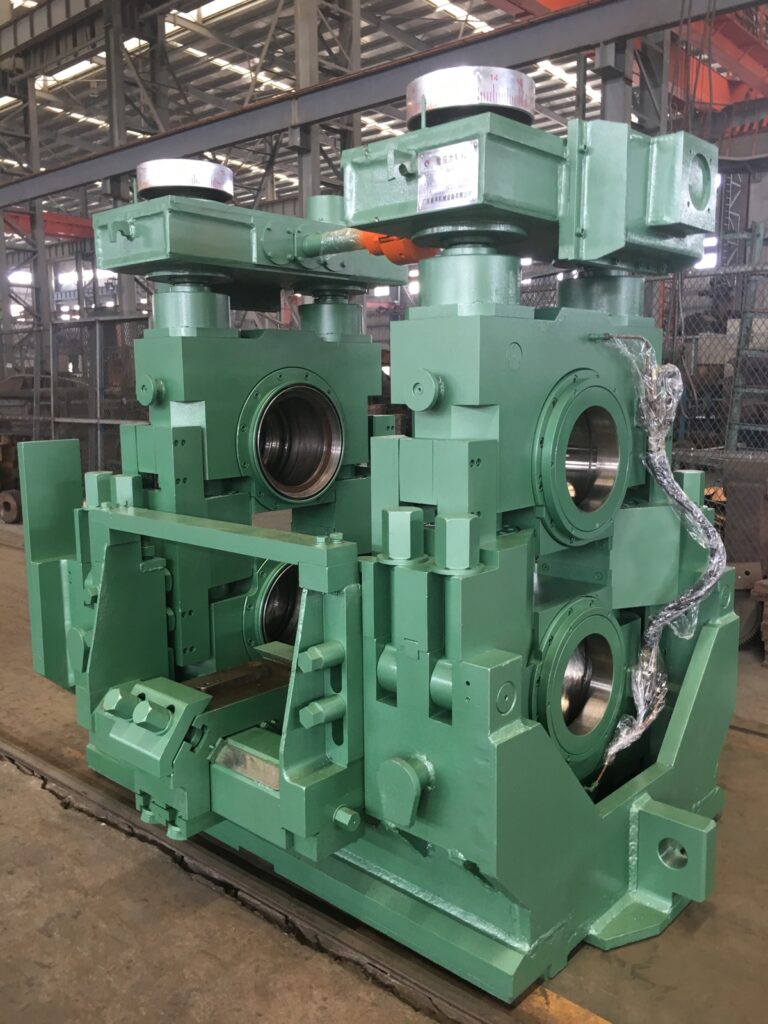
Housingless mill stands offer a radical departure from the heavy frame design. As the name implies, there is no massive outer housing. Instead, the roll chocks are connected directly to each other using sturdy tension bars or screws. The design is compact and significantly lighter.

In this configuration, the chocks and the tension bars form a tight, self-contained stress loop. There is no heavy frame to stretch or bend. The rolls are held in place with hydraulic pre-stressing or mechanical locking systems that eliminate internal movement. This creates a unit that acts as a single, solid block rather than a collection of loose parts rattling inside a frame.

The Hidden Flaws of Conventional Design

You might wonder why you should replace something that is still technically working. The answer lies in the invisible problems that occur during the rolling process. Conventional mill stands suffer from inherent mechanical flaws that are impossible to fix without a complete design change.

The Stretch Factor

Engineers refer to this as “mill spring.” When hot steel enters the roll bite, it exerts a tremendous separating force. It tries to push the rolls apart. In a conventional stand, this force travels through the chocks, the screws, and finally into the tall housing posts.

Because the housing posts are long, they stretch under this load. It acts exactly like a heavy spring. Even a fraction of a millimetre of stretch alters the gap between the rolls. This means the setting you adjusted while the mill was empty changes the moment steel enters the stand. This stretch factor makes it incredibly difficult to maintain consistent gauge control, especially when rolling high-strength alloys.

Hysteresis and Wear

The second major flaw is hysteresis. This is the unpredictable movement caused by the clearances between the chocks and the housing window. For the chocks to slide up and down for adjustments, there must be a small gap. Over time, dust, scale, and heat cause these gaps to widen.

When the load is applied, the chocks shift. When the load is removed, they do not always return to the same spot. This unpredictability creates a “hysteresis loop” where your control system thinks the rolls are in one position, but they are actually in another. This mechanical play leads to accelerated wear on the liners and plates, forcing your maintenance team to constantly shim and adjust the stands just to keep them functional.

5 Reasons to Upgrade to Housingless Stands

The transition from conventional to housingless technology is the single most impactful upgrade you can make to your long product mill. At The Steefo Group, we have seen this transition transform the profitability of numerous plants. Here are five specific reasons why housingless mill stands are the superior choice.

Reason 1: Superior Rigidity

The primary advantage of housingless mill stands is their incredible stiffness. This is due to the shortened “stress path.” In any mechanical structure, the longer the path the force has to travel, the more the material will stretch.

In a housingless design, the tension bars connecting the chocks are very short compared to the tall posts of a conventional housing. This creates a compact stress loop. The result is a stand that is significantly more rigid. When the steel bar hits the rolls, the stand does not yield. It holds its shape against the separating force.

This rigidity ensures that the roll gap remains constant regardless of the load. Whether you are rolling the front end, the middle, or the tail of the billet, the dimension remains stable. This stiffness allows rolling mills to produce strip and long products with tolerances that are impossible to achieve with older frames.

Reason 2: Faster Roll Changing

In the steel business, time is undeniably money. Every minute your mill is stopped for a size change is a minute you are not generating revenue. Conventional stands are notorious for long changeover times. You often have to disassemble parts of the stand, crane out heavy rolls, and manually adjust guides while the line is down.

Housingless mill stands revolutionise this process. They are designed for quick cartridge changes. The entire stand unit, including rolls, chocks, and guides, can be prepared offline in a workshop. When it is time for a change, the operators simply disconnect the drive spindles and fluid lines, lift out the old unit, and drop in the new pre-set cartridge.

This process can reduce changeover times from hours to mere minutes. For a flexible steel plant that handles multiple product sizes in a single shift, this feature alone can increase annual production capacity by a significant margin.

Reason 3: Better Product Tolerances

We touched on rigidity earlier, but let us connect that directly to your product quality. Modern construction projects and automotive manufacturers demand steel with extremely tight dimensional tolerances. They need TMT bars, wire rods, and perfectly uniform sections.

Because housingless mill stands suffer from negligible mill spring, they deliver superior gauge control. You avoid the heavy ends on bars that often occur with conventional stands. This precision reduces the amount of material that gets rejected by Quality Control.

Furthermore, it reduces the give away. When your equipment is not precise, you have to roll slightly on the heavier side to ensure you meet the minimum weight standard. With high-precision housingless stands, you can roll closer to the theoretical minimum weight. This saves a massive amount of raw material over a year, directly boosting your bottom line.

Reason 4: Compact Footprint and Foundation

Space is often a constraint in existing rolling mills. Expanding a line usually involves expensive civil work to reinforce foundations for heavy machinery. Conventional stands require massive, deep foundations to support their weight and absorb the vibrations.

Housingless mill stands are lighter and more compact. Because the stress is contained within the stand itself (the tension bars), less force is transmitted to the foundation. This means they can often be installed on lighter, less expensive foundations.

If you are retrofitting an existing plant, housingless stands are easier to slot into the available space. Their lower height also improves visibility for the operators, making it easier to monitor the rolling process and intervene if necessary. This compact nature simplifies the layout of the mill floor and reduces the initial civil engineering costs for new projects.

Reason 5: Lower Maintenance Needs

As we explained in our detailed guide on rolling mill maintenance best practices, maintenance is the silent killer of mill profitability.. Conventional stands require constant attention. You have to replace wear plates, machine the housing windows, and deal with broken screws or nuts caused by vibration.

Housingless mill stands have fewer moving parts to wear out. The absence of housing liners removes one of the most common maintenance headaches. Since the stand is pre-stressed and rigid, there is less vibration rattling the components.

The bearings in housingless designs also tend to last longer because they are not subjected to the uneven loading caused by chock movement. This leads to a lower Total Cost of Ownership (TCO). While the initial investment might be higher than refurbishing an old stand, the reduction in spare parts consumption and maintenance man-hours pays for the upgrade quickly.

The Economic Case for Upgrading

Deciding to upgrade your mill stands is a financial decision as much as a technical one. To understand the value, you must look at the Return on Investment (ROI).

You can calculate the savings by combining several factors. First, calculate the value of the increased uptime due to faster roll changes. If you gain just 30 minutes of production per day, that adds up to over 150 hours of extra production per year. Second, factor in the reduction in scrap and give away material. Saving just 0.5% of material yield in a high-capacity steel plant translates to millions in savings.

Finally, consider the market demands of 2026. Customers are no longer just looking for steel. They are looking for certified precision. An upgrade to housingless stands positions your mill to bid for high-value contracts that require strict adherence to international quality standards. It future-proofs your facility against rising quality expectations.

Conclusion

The evolution of steel manufacturing is moving relentlessly toward higher precision and efficiency. The era of the massive, flexible conventional frame is fading. In its place, the housingless design has emerged as the standard for modern high-performance rolling mills.

By upgrading to housingless mill stands, you are solving the problems of mill spring and hysteresis that have plagued production for years. You gain superior rigidity, faster changeovers, better product tolerances, a compact footprint, and significantly lower maintenance costs.

At The Steefo Group, we understand that upgrading is a major commitment. However, sticking with outdated technology is a risk that most plants cannot afford to take. The housingless stand is not just a piece of machinery. It is the heart of a profitable, precise, and future-ready rolling operation.

Frequently Asked Questions

1. What is the main difference between housingless and conventional mill stands?

The main difference lies in the frame construction. Conventional mill stands use a heavy outer cast steel housing to hold the roll chocks. Housingless mill stands eliminate this outer frame and connect the chocks directly using tension bars or screws, creating a more rigid and compact unit.

2. Why do housingless stands provide higher rolling precision?

They provide higher precision because they have a shorter stress path. This design significantly reduces “mill spring”, or the stretching of the stand under load. The increased rigidity ensures the gap between the rolls remains constant, delivering tighter dimensional tolerances on the final product.

3. How does upgrading to housingless stands reduce downtime?

Housingless mill stands are designed for rapid cartridge changing. Instead of disassembling the stand on the mill line, operators can swap the entire unit with a pre-assembled replacement in minutes. This offline preparation drastically cuts the downtime required for size or roll changes.

4. Is it difficult to retrofit housingless stands into an existing mill line?

Generally, it is easier than installing new conventional stands. Housingless mill stands have a smaller footprint and are lighter. They require less extensive foundation work, making them ideal for retrofitting into existing layouts without requiring major civil engineering changes.

5. Do housingless stands really lower long-term maintenance costs?

Yes. They eliminate the wear components associated with conventional housings, such as window liners and wear plates. The rigid design reduces vibration, which prolongs bearing life and reduces the frequency of component failure, lowering the overall maintenance burden for the steel plant.

Choose Steefo for High Quality Housingless Mill Stands

In the competitive steel landscape of 2026, your mill’s profitability hinges directly on precision and speed. Stop wrestling with the limitations of outdated conventional equipment and let superior engineering drive your growth. At The Steefo Group, we don’t just supply machinery; we engineer transformation for the modern steel plant. Our advanced housingless designs are built to eliminate mill spring, drastically reduce changeover downtime, and deliver the tight product tolerances that today’s market demands.

Upgrading your line is a strategic investment in your facility’s longevity and performance. With decades of expertise as a leading manufacturer in India, we ensure seamless integration and immediate impact on your bottom line. Don’t let inefficiencies erode your margins any longer. Take the decisive step toward modernisation today. Choose Steefo for High Quality Housingless Mill Stands and experience the difference that world-class engineering makes in your daily production. Contact our team at +91 87589 98607 or write to us at marketing@thesteefogroup.com now to engineer your success.