Buying a wire rod mill is not like buying a machine. It is a chain of linked packages: a reheating furnace, a rolling train, a high-speed finishing block, a laying head, a cooling conveyor and a coil handling line, each of which must pass a hot, fast-moving strand to the next without a hiccup. A turnkey wire rod mill plant puts one contractor in charge of that entire chain, so it is worth understanding exactly what that promise covers before you sign anything.
A turnkey wire rod mill plant is a complete coil-producing rolling line supplied by a single contractor, who designs, manufactures, installs and commissions every section from the billet reheating furnace to the coil handling system, then hands over a plant that runs to the agreed output, rod sizes and quality.
The word “turnkey” is used loosely in this industry. Some offers include civil design input, utilities and automation; others cover only the rolling equipment and leave the interfaces to you. This guide sets out what a genuine scope should include, how the project unfolds from contract to first coil, and how to judge a contractor before money changes hands. It is written for plant owners, project heads and procurement teams who are comparing options.
Turnkey Wire Rod Mill Plant at a Glance
- Scope: a real turnkey scope runs from billet receipt to packed coil and names who owns utilities, automation and the join between the mill train and the rod outlet.
- Timeline: one published large high-speed mill reached first coil 19 months after contract signature, so ask for a milestone chart, not a single delivery date.
- Contractor: insist on a written performance guarantee with test conditions, a reference line you can visit and one party responsible for interfaces.
- India: plan IS 7887 and BIS certification for your rod from the start.
What Does “Turnkey” Mean for a Wire Rod Mill?
Under a turnkey contract, one party is responsible for design, manufacture, supply, erection, commissioning and proof of performance. You receive a working plant rather than a set of machines. That is different from equipment-only supply, where you buy the machines and take on the job of integrating them, and from EPC or EPCM models, where a contractor or manager coordinates several separate suppliers on your behalf. Our guides on EPC vs EPCM vs turnkey solutions and turnkey vs traditional solutions compare these models in general terms. This section looks at what is specific to wire rod.
A wire rod line is unforgiving about interfaces. Published designs for large mills quote guaranteed finishing speeds of around 100 metres per second and above. At that speed, a small mismatch between neighbouring packages shows up immediately as coil defects or stoppages. Examples are a pinch roll that does not suit the finishing block, or a cooling section that does not suit the laying head. That is the strongest argument for a single point of responsibility.
It is also worth knowing that wire rod projects are often split in practice. In several publicly announced contracts, the rod outlet, which covers everything from the exit of the last main mill stand to the coil reforming station, was ordered as a separate package from the main mill train. A 2011 contract for two single-strand mills is one example. A split can work, but if the packages come from different suppliers, the responsibility for the join between them moves onto you.
| Question | Single turnkey contractor | Split packages (mill train and rod outlet) |
|---|---|---|
| Who is responsible for the interface between packages? | The contractor | You, or a consultant you appoint |
| Who guarantees the final rod quality and output? | One party, against one performance test | Each supplier guarantees only its own section |
| Schedule coordination | One master schedule | Several schedules to align |
| Spares and after-sales | One supplier and one parts list | Separate lists and support channels |
| Your internal effort | Lower | Higher |
Scope of Supply: What Does a Complete Wire Rod Plant Include?
A complete turnkey wire rod production line takes billet in at one end and delivers packed coils at the other. Published scope descriptions from major equipment suppliers are consistent about the main blocks, and they also list the supporting items that buyers often forget to price: hydraulic and lubrication systems, power supply, automation, water treatment, compressed air and roll shop facilities.
Reheating Furnace and Rolling Train
The line starts with billet handling and a reheating furnace sized to feed the mill without starving it. Published projects quote billets of roughly 130 to 200 mm square. After reheating, the billet passes through descaling and then the roughing and intermediate stands, which reduce the section in stages. Some modern lines use housingless stands in these sections. Loopers hold the strand between stands to control tension, and shearing machines crop the head and tail ends and cut up the bar if a pass goes wrong.
Finishing Block and Rod Outlet
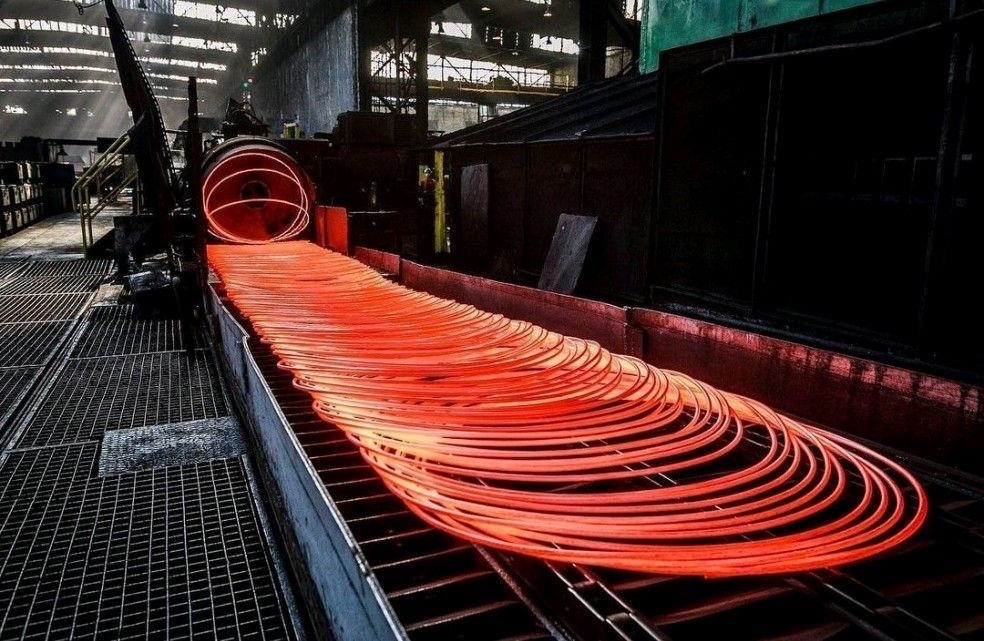
This is the heart of a wire rod line. The finishing block rolls the strand to its final diameter at very high speed. Published designs use blocks of eight to ten passes, typically on a common drive, and rod sizes commonly range from 5.5 mm to 16 mm, with some lines reaching about 25 mm. After the block, a pinch roll controls the strand, the laying head forms it into rings, and water boxes and a controlled-cooling conveyor set the rod’s microstructure. If you want the process detail, our explainer on the wire rod mill walks through each step.
Coil Handling and Packaging
Rings of rod are collected into coils, compacted, tied, weighed and tagged before dispatch. Coil weights of around two to two and a half tonnes appear in published designs. The coil handling line must keep pace with the rolling speed, because a slow coil station backs up the whole outlet.
Utilities, Electrics and Automation
The least glamorous part of the scope is often where projects run into trouble. Water treatment and cooling water circuits, compressed air, hydraulics, lubrication, power distribution, drives, instrumentation and the automation system that cascades speed between stands all need a clear owner. Publicly announced wire rod contracts often spell these out, including water treatment, compressed air and roll turning shop facilities, which tells you they belong in the scope discussion from day one.
| Section | Main equipment | What to confirm in the offer |
|---|---|---|
| Billet handling and reheating | Charging, reheating furnace, burners, fuel system | Furnace capacity against mill output, fuel type, hearth design |
| Rolling train | Roughing and intermediate stands, shears, loopers, guides | Stand type, number of stands, pass design, drive type |
| Finishing block and rod outlet | Finishing block, pinch roll, laying head, water boxes, cooling conveyor | Rated speed, rod size range, dimensional tolerance |
| Coil handling | Coil forming, compactor, tying, weighing, tagging | Coil weight and handling rate against line speed |
| Utilities and electrics | Water, air, hydraulics, lubrication, power, drives, automation | Who supplies, who connects, where your responsibility starts |
| Services | Erection, commissioning, training, spares | Team size, duration, recommended spares list |
How Long Does a Turnkey Wire Rod Mill Project Take?
A turnkey wire rod rolling mill plant follows a sequence of stages, and the order matters because several of them overlap:
- Basic engineering and layout freeze. Capacity, rod sizes, billet size and plant layout are fixed.
- Detail engineering. Drawings, foundation loads and utility requirements are issued.
- Manufacturing and shop testing. Equipment is built and checked at the contractor’s works.
- Civil works. Foundations and buildings are prepared, usually in parallel with manufacturing.
- Shipment and erection. Equipment is installed on site.
- Cold commissioning. Utilities, drives, interlocks and input-output checks are completed without steel.
- Hot commissioning. The first billets are rolled and the first coil is produced.
- Ramp-up, performance test and acceptance. The mill is run to prove guaranteed output and quality, and acceptance certificates are issued.
- Handover and training. Operators and maintenance teams are trained and the plant is handed over.
Published examples show how wide the range is. One large two-strand mill of 750,000 tonnes a year, supplied to a European producer, reported its first coil 19 months after contract signature in 2018. A seven-week hot-test period followed, in which 25,000 tonnes of rod were produced. In a 2009 example, the electrical commissioning of a complete twin-strand mill, from input-output tests through to production, took two months. Taken together, they show that most of the elapsed time goes into engineering, manufacture and site readiness, while commissioning takes weeks to a couple of months. Your own timeline depends on mill size, the contractor’s workload and how ready your site is, so ask for a milestone chart with dates against each stage, not a single delivery promise.
A phased approach is also possible. A published project paper on one turnkey rod and bar mill describes the wire rod outlet as a second phase of hot commissioning, fed from the bar mill’s finishing stands. Another published rod outlet contract scheduled hot commissioning in four phases. If you already run or plan a TMT bar line, leaving space and utility capacity for a future outlet at the layout stage keeps that option open, and our TMT rolling mill setup guide covers the wider planning questions. Delays can also come from site readiness, such as late foundations, power connection approvals and billet supply for hot trials, and not only from the equipment itself.
How to Choose a Turnkey Wire Rod Mill Contractor
You will see suppliers described as a turnkey wire rod rolling mill plant contractor, a wire rod mill turnkey engineering firm or a complete wire rod rolling mill plant solution provider. The label matters less than the evidence. Can they show they have delivered and commissioned a line like yours? Will they put their guarantees in writing? Use the checklist below to compare offers on equal terms.
Contractor Evaluation Checklist
| Criterion | What to ask | Why it matters |
|---|---|---|
| Performance guarantee | Which output (tonnes per hour), rod sizes, tolerances and yield are guaranteed? How long is the test and under what conditions? | A guarantee without test conditions is hard to enforce |
| Critical equipment source | Which items are made in the contractor’s own works: finishing block, laying head, stands, gearboxes? | In-house manufacture shortens lead times and keeps design knowledge with the supplier |
| Interface responsibility | Does one party own the join between mill train and rod outlet? | Most coil quality problems start at interfaces |
| References | Can you visit a running wire rod or block mill they supplied? | Operating lines prove more than brochures |
| Automation and drives | Who designs and commissions speed and tension control? | Speed cascade control decides dimensional stability |
| Commissioning and training | How many engineers, for how long, and how are operators trained? | Ramp-up quality depends on the people on site |
| Spares and after-sales | Is a recommended spares list included, with agreed lead times? | The first breakdown tests the relationship |
| Schedule commitments | Are milestones and delay remedies written into the contract? | Without them, the schedule is only an estimate |
Indian buyers should also raise product compliance early. Mild steel wire rod for general engineering purposes is covered by IS 7887:1992, and the BIS standards portal lists certification for this standard as mandatory, with its quality control order shown as implemented on 18 March 2016. Confirm the current licensing position with BIS before commissioning, so that your first production runs can be certified and sold.
Questions to Ask Before You Sign
- What exactly is the scope boundary, from billet receipt to packed coil?
- Which utilities and civil items are yours, and which are the contractor’s?
- What output, rod size range and tolerance are guaranteed, and how will they be tested?
- What happens if the guarantee test fails?
- Which equipment is manufactured in house and which is bought in?
- Who is responsible for the interface between the mill train and the rod outlet?
- What is the milestone schedule, and what remedies apply to delays?
- How many commissioning engineers will be on site and for how long?
- How will our operators and maintenance staff be trained?
- What spares are included in the price, and what are the lead times for the rest?
- Can we visit a comparable running line?
- What support is available after handover?
Red Flags
- A “turnkey” price that excludes utilities, automation or commissioning without saying so.
- A performance guarantee with no test procedure.
- No reference line you can visit.
- A single delivery date with no milestone chart.
- Reluctance to name who is responsible for interfaces.
For a view of how budgets are usually structured, see our cost breakdown of a turnkey rolling mill project.
Where Steefo’s Wire Rod and Block Mill Range Fits
The Steefo Group designs and manufactures rolling mill equipment at its facility in Changodar, Ahmedabad, and has spent more than four decades on rolling mill design, manufacturing and turnkey project execution. For wire rod and TMT lines, its wire rod block mill range covers side loopers, shears, block stands, coil laying heads, coil cooling conveyors, coil handling systems, entry and exit guides, bevel gearboxes, optical guide setters, lubrication systems, water boxes and high-speed pinch rollers. These are the items that sit at the centre of the scope table above.
Steefo’s wider turnkey solutions for steel plants combine design, manufacture and project execution under one team. If you are looking for a wire rod rolling mill total plant solution, whether a new line or a rod outlet added to an existing mill, share your target output, rod size range and billet size with our engineering team for a scope discussion.
A turnkey wire rod mill plant is only as good as its scope, its guarantees and the contractor behind them. Define the boundary from billet to packed coil, make one party responsible for the interfaces, insist on a written performance test, and compare offers against the same checklist. Buyers who do this are far less likely to meet surprises at hot commissioning.
Frequently Asked Questions
What is included in a turnkey wire rod mill plant?
A turnkey wire rod mill plant normally includes the reheating furnace, rolling train, finishing block, pinch roll, laying head, controlled-cooling conveyor and coil handling line, plus utilities, electrics, automation, erection, commissioning and training. The exact boundary should be written into the contract, because some offers exclude civil works or utilities.
How long does it take to set up a turnkey wire rod production line?
It varies with size and site readiness. One large two-strand mill reported its first coil 19 months after contract signature, followed by a seven-week hot-test period. Smaller lines will differ. Ask your contractor for a milestone schedule that covers engineering, manufacturing, erection, commissioning and acceptance.
What is the difference between turnkey and EPC for a wire rod mill?
In a turnkey contract, one contractor designs, supplies, installs and commissions the plant and guarantees its performance. In an EPC or EPCM arrangement, a contractor or manager coordinates separate suppliers, so responsibility for the interfaces and the overall guarantee can be more divided.
What should a performance guarantee for a wire rod mill cover?
It should state guaranteed output in tonnes per hour, the rod size range, dimensional tolerance and yield, along with the test duration, billet quality and operating conditions. It should also say what remedies apply if the mill misses the guaranteed figures.
Is BIS certification mandatory for wire rod made in India?
Mild steel wire rod for general engineering purposes is covered by IS 7887:1992, and the BIS standards portal lists certification for it as mandatory. Confirm the current licensing requirements with BIS before commissioning so that your first production can be certified.
Does Steefo supply wire rod mill equipment and turnkey projects?
Yes. Steefo designs and manufactures wire rod and block mill equipment and executes turnkey rolling mill projects from its facility in Changodar, Ahmedabad. Send your capacity, rod sizes and billet details to our engineering team to discuss the scope for your plant.
Get in Touch
To discuss a turnkey wire rod mill plant, contact The Steefo Group’s engineering team, call +91 98240 76873, or write to marketing@thesteefogroup.com with your target output, rod sizes and billet size.
Sources
- Bureau of Indian Standards, IS 7887:1992, Mild steel wire rod for general engineering purposes (BIS Know Your Standards).
- Danieli, Excellent startup for Pittini’s Acciaierie di Verona new high-speed wirerod mill.
- AIST Steel News, Siemens to Provide Rod Outlets to Lianfeng Steel for Single Strand Wire Rod Mills (2011).
- AIST Steel News, AIC Commissions Wire Rod Plant for Univers Acier (2009).
- Schultz, A. R., Silat selects Russula to engineer and supply a 700,000 tpy steel plant, 52nd Rolling Seminar, ABM, 2015.